
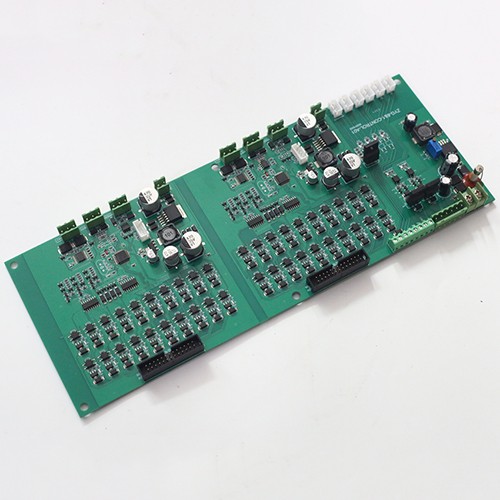
Industrial control box assembly processing
- PCB board: Ensure that the quality and design of the PCB board meet the requirements of the industrial control box.
- Electronic components: Prepare the required electronic components according to the BOM (Bill of Materials), including DIP plug-ins, SMT patch components, etc.

Four-port WIFI gateway PCBA
- Quad-port WIFI gateway PCBA generally refers to the printed circuit board assembly of a WIFI communication gateway with four network interfaces. This type of equipment is widely used in scenarios that require multiple network connections and data transmission.
Box Build and Final Product Assembly
Boards rarely ship alone. Somewhere between the assembly line and the end customer there is an enclosure, a set of cables, a display, a firmware version and a carton, and every one of those steps is a place where a good board turns into a bad product. Box build takes that sequence into the same factory that made the board.
What the box build stage covers
- Cable and harness assembly to drawing, including crimping, soldering, sleeving and continuity check.
- Mechanical integration: fitting the PCBA into the enclosure, adding displays, switches, connectors, standoffs, thermal interface material and hardware.
- Firmware and software loading with version control, so the unit record shows what was programmed.
- Functional test of the complete unit against an agreed procedure and fixture, including power-up, load, interface and, where relevant, burn-in.
- Labelling, serialisation and packaging, with barcodes and regulatory marks applied and recorded.
Why unit-level test earns its place
A board that passes functional test on its own can still fail as a unit, and the reasons are usually mechanical or thermal rather than electrical. A connector that is intermittent once the harness is under tension, a grounding path that changes when the board is screwed to a metal chassis, or a regulator that has adequate margin on the bench and none inside a sealed case all pass board-level test and fail in the field. Testing at the level the customer ships at catches them in the factory, where the cost of fixing them is contained.
Packaging for export
Much of our box build work ships to Europe, Russia and the Americas, so packaging is specified for air freight and onward distribution rather than for local delivery: foam or moulded inserts, moisture protection where the product or the climate requires it, and carton markings that match the customer requirements for handling, orientation and traceability. Packaging is a small share of the total cost and the most visible part of the delivery, which makes specifying it early worthwhile.
How a box build programme starts
Send the assembly drawing, the bill of materials for the complete unit, the firmware version and the test specification if one exists. Where a test procedure does not exist, it can be developed alongside the first build. Because the board itself is built in the same factory, the box build stage shares one material plan and one set of milestones with PCBA manufacturing rather than being a separate order with its own schedule.
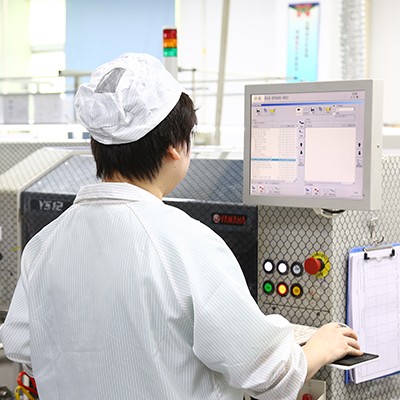
- Factory environment
Why choose us?
Beyond the assembled board, Kilandu builds the finished unit: cable and harness assembly, mechanical integration, functional test of the complete product, labelling and packaging that survives an air freight journey to Europe, Russia or the Americas.
Application
Each application area has its own assembly requirements. What changes from a medical instrument to a motor drive is the process, the acceptance class and the design rules that matter, and the pages below set out what is different about each one.